Zinc Spray
Metal spraying, also called thermal spraying, protects products in harsh environments and greatly extends their life. It's used wherever a coating is vital to how long something lasts.
Anti-corrosive finishing
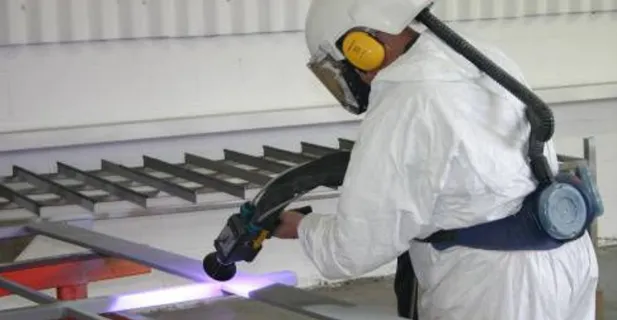 Metallised coatings fall into two broad groups: finishing coatings, such as anti-corrosion and decorative coatings, and engineering coatings, such as wear-resistant and thermal barrier coatings.
Metal spraying is widely used in oil and gas, construction, petrochemical and marine work, where corrosion is a constant problem. There are four main thermal spray processes: flame spray, arc spray, plasma spray and high velocity oxygen fuel (HVOF). Flame spray and arc spray are the two normally used for finishing coatings.
How it works
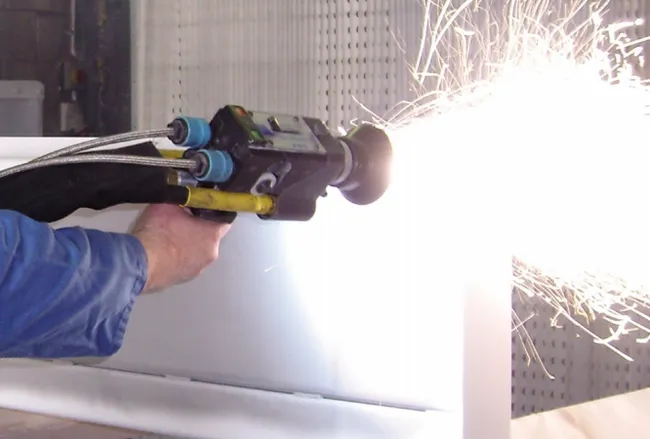
Every thermal spray method projects small molten particles onto a prepared surface, where they build up into a continuous coating. That needs three things: a heat source, the coating material, and a way of atomising and projecting it. When the particles hit the surface they flatten, freeze and bond, first to the roughened steel and then to each other as the coating builds up.
The molten particles carry very little heat compared with the part being sprayed, so the part itself usually stays well below 100°C. That means there's normally no heat distortion, which is a big advantage over hot-dip galvanising.
Wire flame spray
Most anti-corrosion coatings are applied by wire flame spray. A wire is fed through an oxygen-propane flame, where it melts, and a jet of compressed air atomises the molten metal and blows it onto the work. The wire is driven through the spray gun by an air motor and gearbox. Standard wire diameters range from 1.6mm to 4.76mm (1/16" to 3/16"), supplied on coils or in drums.
Zinc spray or galvanising?
Hot-dip galvanising means dipping the steel in a bath of molten zinc at around 450°C. It works well, but the size of the bath limits what can be done, and large, thin or complicated fabrications can warp in the heat.
Zinc spray avoids both problems. There's no bath to fit into and the steel stays cool, so it's a good choice for:
- long or large fabrications that won't fit in a galvanising bath
- thin or complex steelwork that could distort in molten zinc
As with any coating, preparation matters. Steel is shot blasted first, which gives the sprayed zinc a rough surface to grip.
Getting a quote
Let us know the sizes and quantities, where the steel will be used, and any coating specification you've been given. Photos or drawings help too, so mention them when you send us a message.